
Two rolls come back from inspection with the same Ra. On paper they’re twins, so you set them up the same way and start the run. One lays down a perfect coat. The other starts leaving voids halfway through the job. Disaster. So why can two rolls with the same Ra behave nothing alike on press?
Usually, one roll is evenly fine all over and the other is smooth apart from a few deep pits. Ra, the surface roughness number most people check, quietly averages those pits away. Rz doesn’t, and that’s the whole reason it exists.
Here’s how the two differ, and when to use each.
What is surface roughness?
Run a fingernail across a newly polished roll and it feels perfectly smooth. Put it under a microscope and it’s a mountain range. Surface roughness is simply a way of putting numbers on those peaks and valleys.
To measure it, a device traces a line across the surface, or maps a whole patch of it, and records the height at every point. Software then draws a line through the middle, called the mean line, and works out how far the surface rises above it and dips below it.
How small are we talking? A human hair is roughly 50 to 100 µm thick. The roughness on a coated roll is often a few microns, sometimes less. You’d have to split that hair twenty ways to get close.
Not everything counts, though. Long, gentle waves across the surface, left by vibration during machining for example, are filtered out so that only the fine texture is measured. That filter is one reason two devices set up differently can give different numbers for the same surface.
What is Ra?
Ra is the average, and it’s the number almost everyone checks first. Take every point on the profile, measure how far it sits from the mean line, above or below, and average the lot. Older drawings call it CLA (centre line average) or AA (arithmetic average). It’s the most widely used roughness number, and the standard in North America.
Think of a swimming pool. Ra tells you its average depth, which is handy and easy to compare from week to week. But a pool that averages 1.5 metres can still have a 4 metre deep end, and the average won’t breathe a word about it.
That’s Ra in a nutshell. One scratch or pit barely nudges it, so it’s great for tracking slow wear and hopeless at catching faults.
What is Rz?
Rz goes straight for the deep end. A typical trace is split into five equal sections. In each one, the height from the highest peak to the lowest valley is measured, and Rz is the average of those five heights. This is Rz as defined in ISO 4287 and ISO 4288, and the same as the older German DIN Rz.
Try it. Drag the stylus along the profile and watch both numbers. Then add one deep pit and see how the numbers change.
Because it’s built from the extremes, Rz picks up the marks that cause trouble on press, like a pit in a base coat or a scratch in chrome. It’s the standard figure across most of Europe.
Is Rz always bigger than Ra? On the same surface, yes, and usually by several times. Rz measures the full drop from peak to valley, while Ra only measures the average distance from the middle.
One trap worth knowing about. Older Japanese standards (JIS B 0601:1994) used a different Rz, based on the five highest peaks and the five deepest valleys. It’s now called RzJIS. If a number comes from a Japanese supplier, check which Rz they mean before you compare.
Ra vs Rz: which should you use?
Neither wins on its own. They answer different questions: Ra tells you the trend, and Rz tells you the risk.
| Ra | Rz | |
|---|---|---|
| What it measures | Average height from the mean line | Average peak-to-valley height |
| Effect of one deep mark | Small | Large |
| Best for | Tracking gradual wear, comparing like surfaces | Catching faults, checking a surface before coating |
| Where it is most used | North America | Most of Europe |
Use Ra to follow a surface over time. A coating or embossing roll that wears slowly between refurbishments shows up as a gradual change in Ra, which is easy to chart.
Use Rz when one fault can wreck the job. Checking a nickel base coat before laser engraving is the classic example: one deep pit is enough to scrap the cylinder, and Ra would barely notice it.
Most of the time, measure both. It’s no extra effort, and customers on both sides of the Atlantic get the number they’re used to.
Can you convert Ra to Rz?
Short answer: not reliably, whatever the charts say. Search for an Ra to Rz conversion and you’ll find ratios of four to seven for typical machined surfaces, and some as high as twenty.
That spread is the giveaway. The ratio depends on the shape of the surface. Back to the pool: two pools can share the same average depth and have completely different deep ends. Knowing the average won’t tell you which one is safe to dive into.
A ratio does have one use, as a quick sanity check. If your Rz is much more than seven times your Ra, something odd is going on in the profile and it’s worth a closer look. But if a customer asks for Rz, measure Rz.
Beyond Ra and Rz: skewness, kurtosis and peak count
Ra and Rz tell you how rough a surface is. What they don’t tell you is the shape of that roughness, and when you’re coating, shape matters a lot.
Rsk (skewness) tells you whether a surface is mostly peaks or mostly valleys. Negative means a flat top with valleys cut into it, which holds coating and ink well. Positive means sharp peaks sticking up, and those are the first to go.

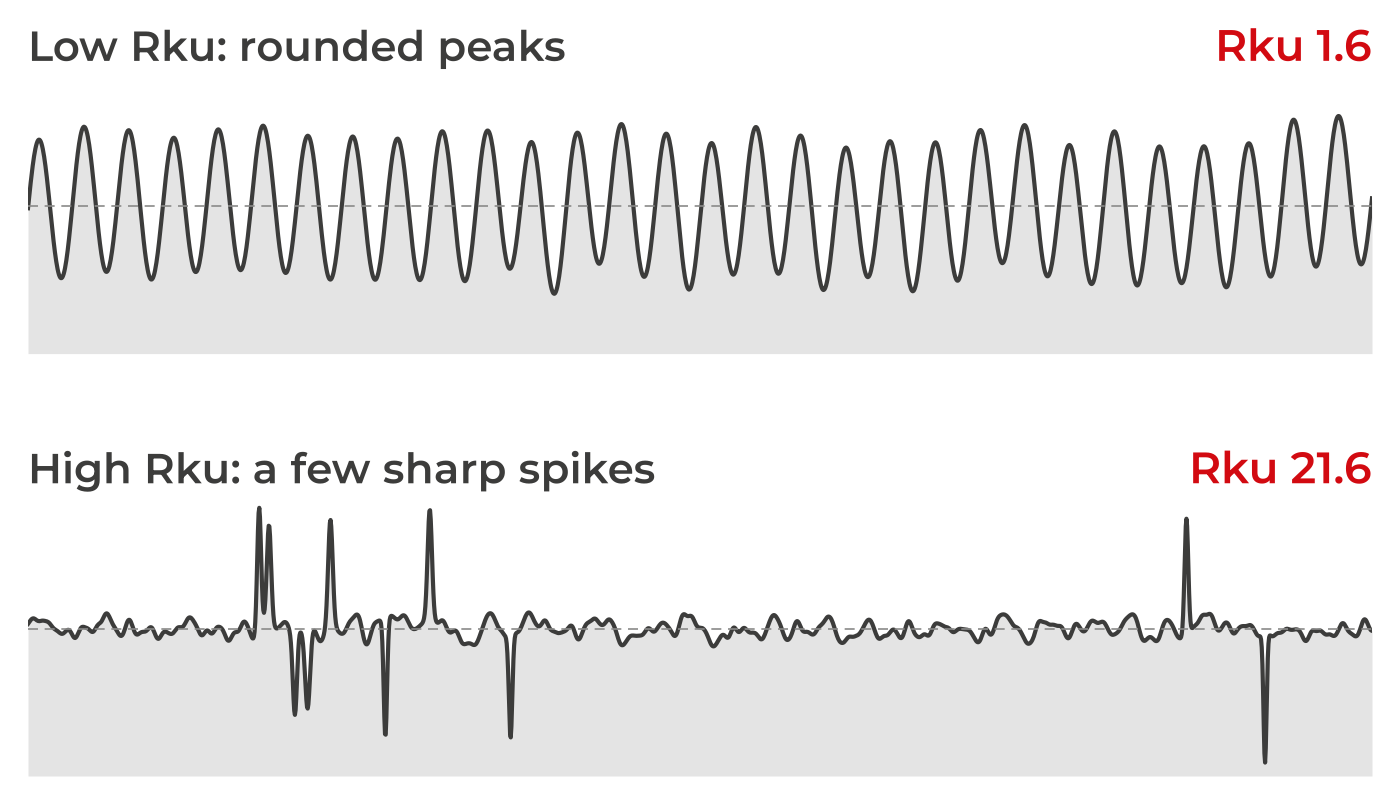
Rku (kurtosis) tells you how sharp those peaks and valleys are. A rounded, even texture scores low. A surface with a few sharp spikes scores high. Those spikes wear quickly at first, and they’ll happily wear down anything that runs against them.
RPc (peak count) is the number of peaks per centimetre. Two surfaces with the same Ra can take a coating very differently if one has twice as many peaks.
How to measure surface roughness
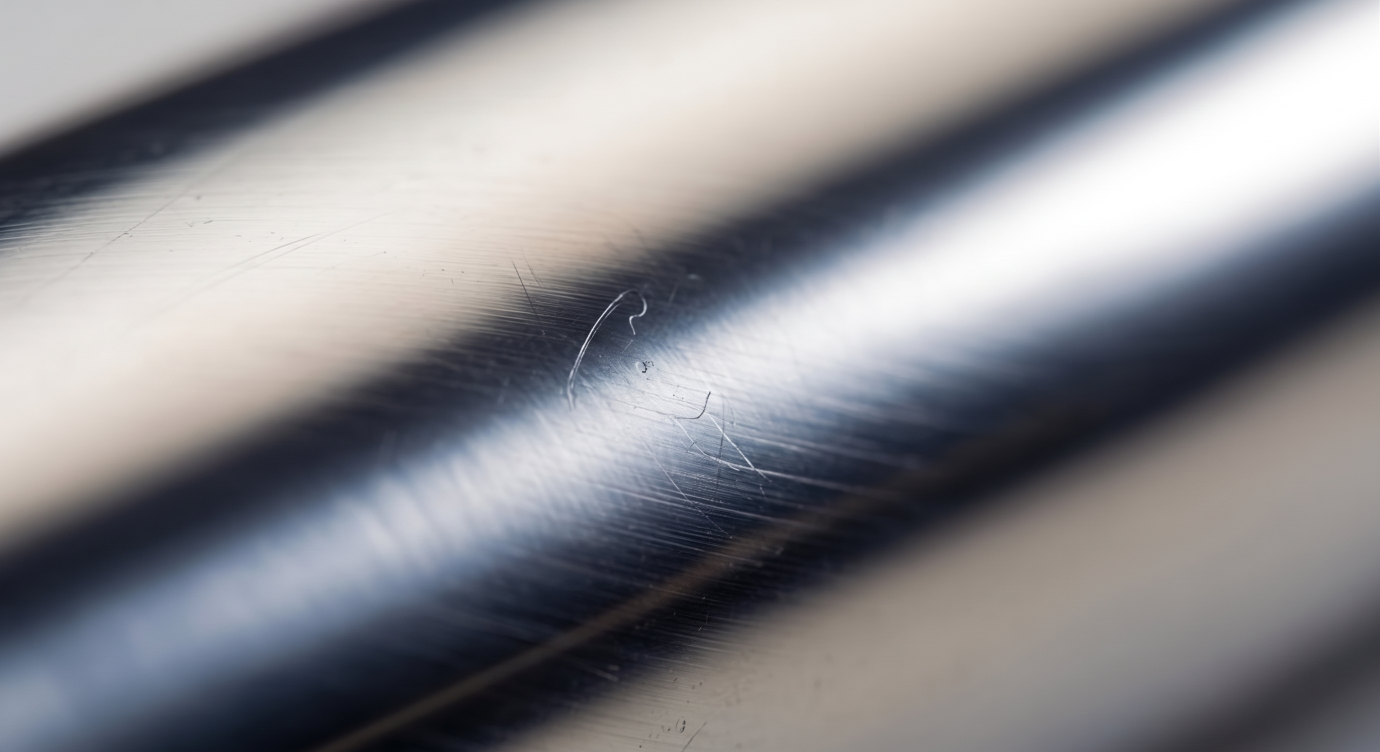
The traditional tool is a stylus profilometer: a diamond-tipped needle dragged across the surface, rising and falling like the needle on a record player. Here’s the catch. It measures by touching, and the surface it’s touching is usually the one you’re trying to protect. On a soft coating, fresh plating or a finished cylinder, that needle can leave a scratch of its own. Not ideal on a cylinder you’re about to print with. It also reads just one thin line, so a fault a few millimetres to the side goes unseen.
Optical 3D measurement doesn’t touch the surface at all, so there’s nothing to damage. It maps a whole area rather than a single line, so one scan shows where a fault is as well as how deep it goes. And you can come back to the same spot weeks later to see what’s changed.

Surface roughness in printing and coating
In printing and converting, roughness decides how well a surface takes a coating and how evenly it lets it go. The trouble is that getting it wrong tends to show up late. A cylinder that fails after engraving because nobody checked its base coat has already eaten machine time and material. A substrate that’s too rough or too smooth causes trouble through the whole run, and the cause is rarely traced back to the surface.
Measured at the right moment, roughness is one of the cheapest checks you can make. A fault found at measurement costs minutes. The same fault found on press costs a run.

Measuring Ra and Rz with Troika
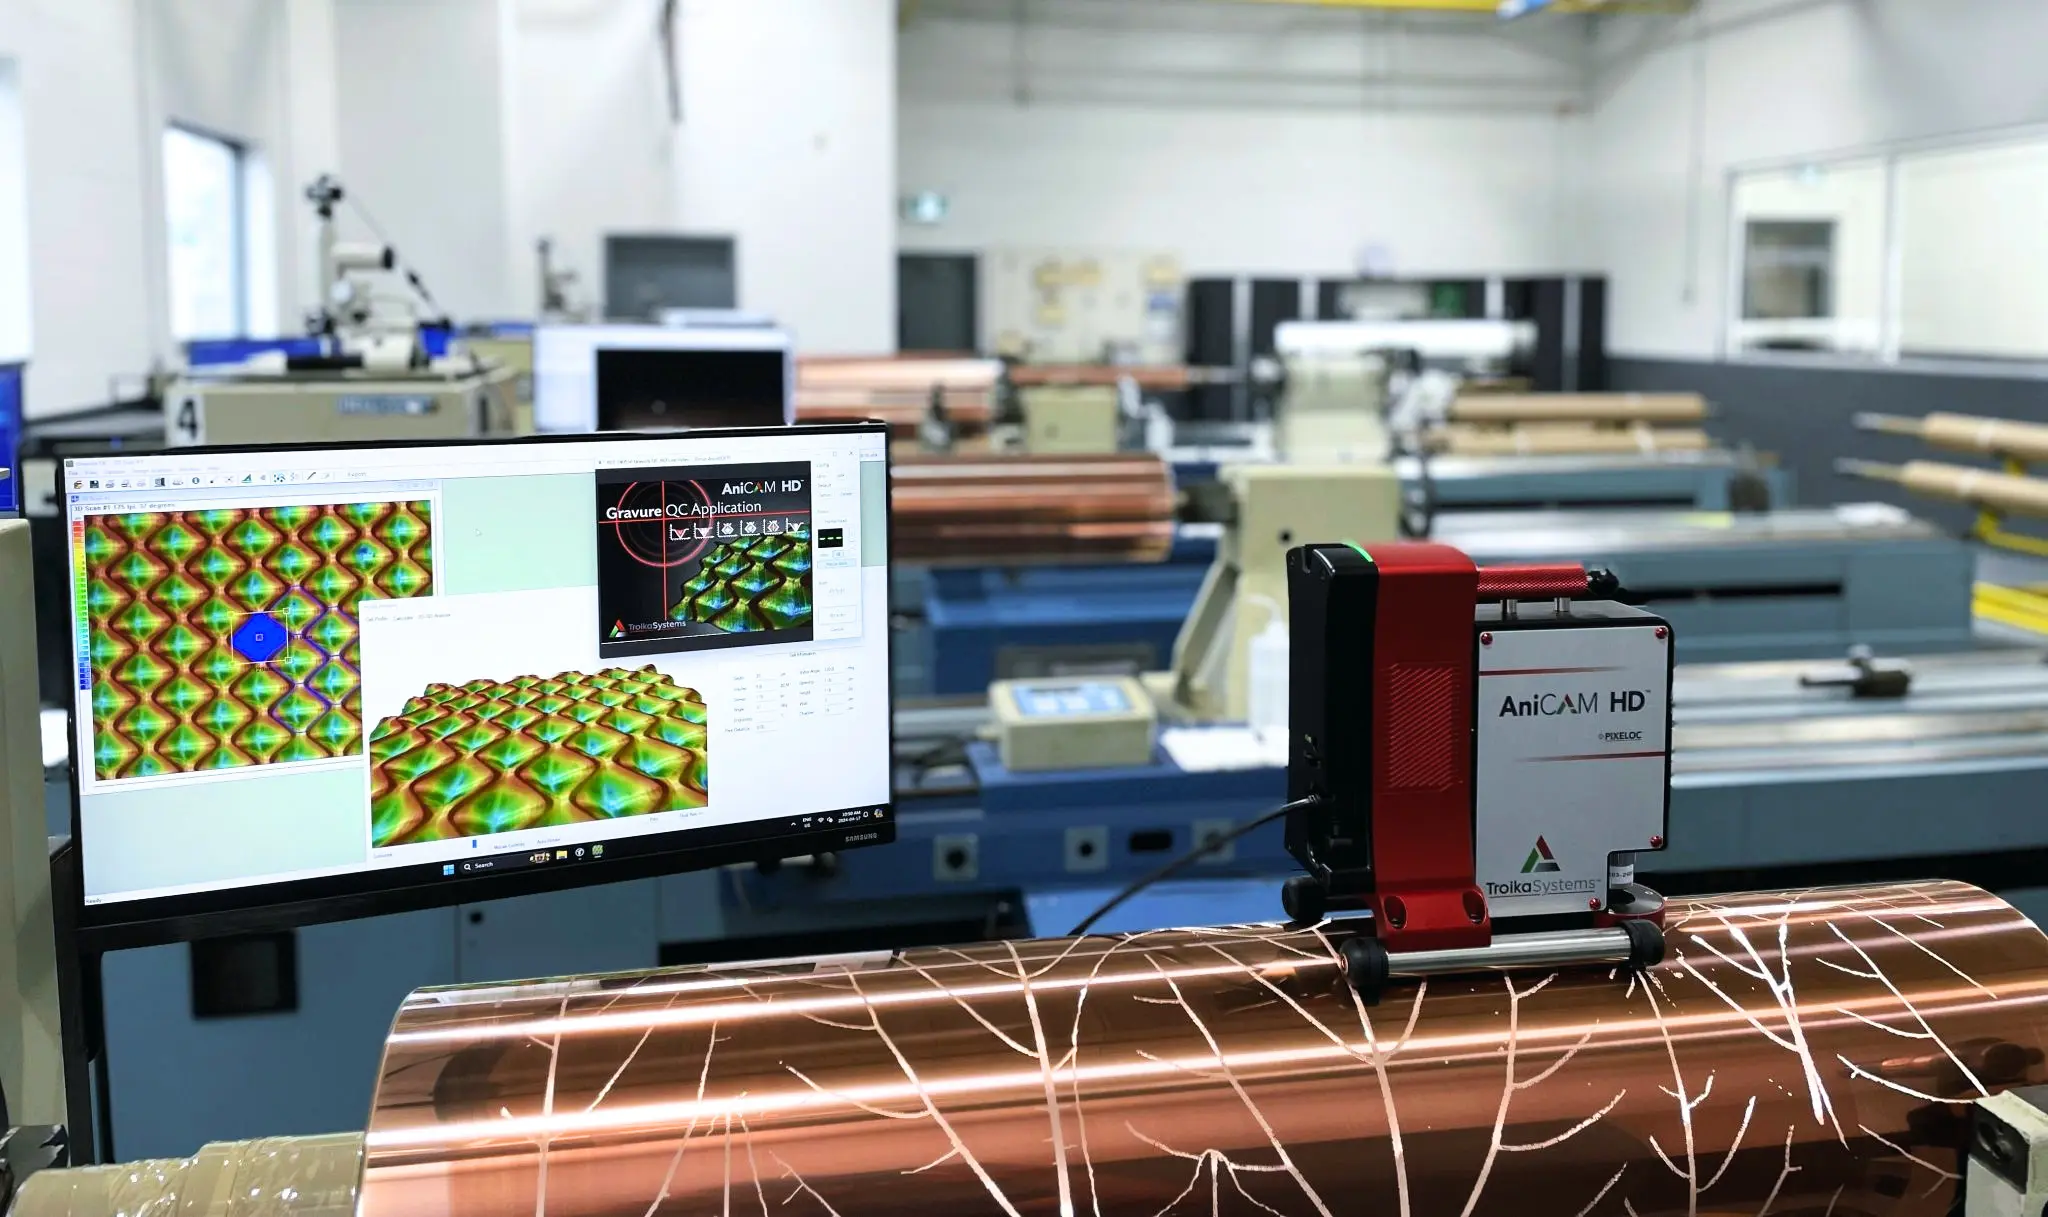
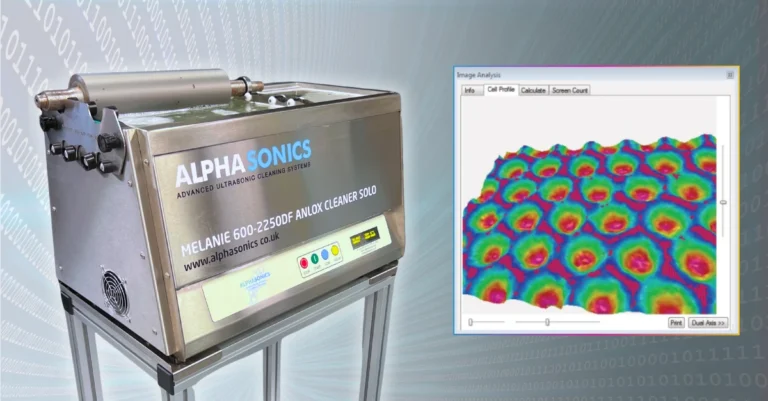
Our Surface Roughness software measures Ra, Rz, RPc, Rsk and Rku from a single 3D scan, accurate to about 1 µm. It comes with every Troika EVO and works with SurfaceCAM HD, our 3D microscope for low-screen anilox, coating and embossing rolls.

Click any point on the scan and the numbers update straight away. Working to a limit that was set with a stylus? A stylus-style filter (5 µm as standard, adjustable from 1 to 100 µm) gives you a matching reading, without anything ever touching your roll. Individual and average results sit side by side.
Track Ra, Rz and RPc over the life of a roll or cylinder and you’ll see wear building long before it costs you a run or a re-engrave.
If you can’t measure it, you can’t control it. Request a demo to see what your surfaces are actually telling you.